Cold Chain Packaging That Maintains Containment
Food grade shrink wrapping equipment in Battle Creek for processing lines operating under refrigerated and sanitary conditions
When beverage multipacks exit a shrink tunnel or pallet loads enter cold storage at 34°F, standard stretch films become brittle and snap under tension, and non-food-grade adhesives contaminate product contact surfaces. BRAVO SYSTEMS INC handles food grade shrink wrapping equipment and cold-temperature packaging materials for facilities producing cereal, snack foods, bottled beverages, and refrigerated ready-to-eat products where FDA compliance, line speed, and temperature performance determine whether packaging succeeds or generates downtime. Battle Creek's concentration of food processing plants—many operating in buildings constructed during the mid-20th century with retrofitted clean rooms and updated HVAC but original floor plans—requires packaging systems that fit constrained spaces, integrate with legacy conveyors, and meet current sanitary design standards.
The process involves cold-temperature stretch films formulated to retain elasticity and cling below 40°F, stainless-steel case sealers with tool-free teardown for wash-down between product runs, shrink tunnels with precise heat control to avoid package distortion or uneven sealing, and automated palletizing that maintains load stability through cold storage and refrigerated truck transport. Food safety regulations require that all packaging materials in direct or indirect product contact meet FDA compliance for food use, and that equipment surfaces in the packaging zone allow cleaning without harboring bacteria or product residue.
Schedule a sanitary packaging evaluation to review material compliance, equipment cleanability, and cold-chain performance for your production environment.
How Cold Storage Packaging Addresses Containment Failure
Cold storage packaging failure shows up as film that cracks and separates from the load, shrink film that doesn't conform tightly after tunnel exit, and case sealer tape that loses adhesion on cold corrugated surfaces. These failures occur because conventional films and adhesives are formulated for ambient temperature application and lose performance when substrate temperature drops below their glass transition point or when thermal contraction exceeds material elongation limits.
After cold-capable materials and equipment are installed, you'll notice pallets that exit the cooler with full wrap integrity, beverage multipacks with uniform shrink coverage and no loose ends, and sealed cases that remain closed through freezer storage and thaw cycles without tape lifting or flap separation.
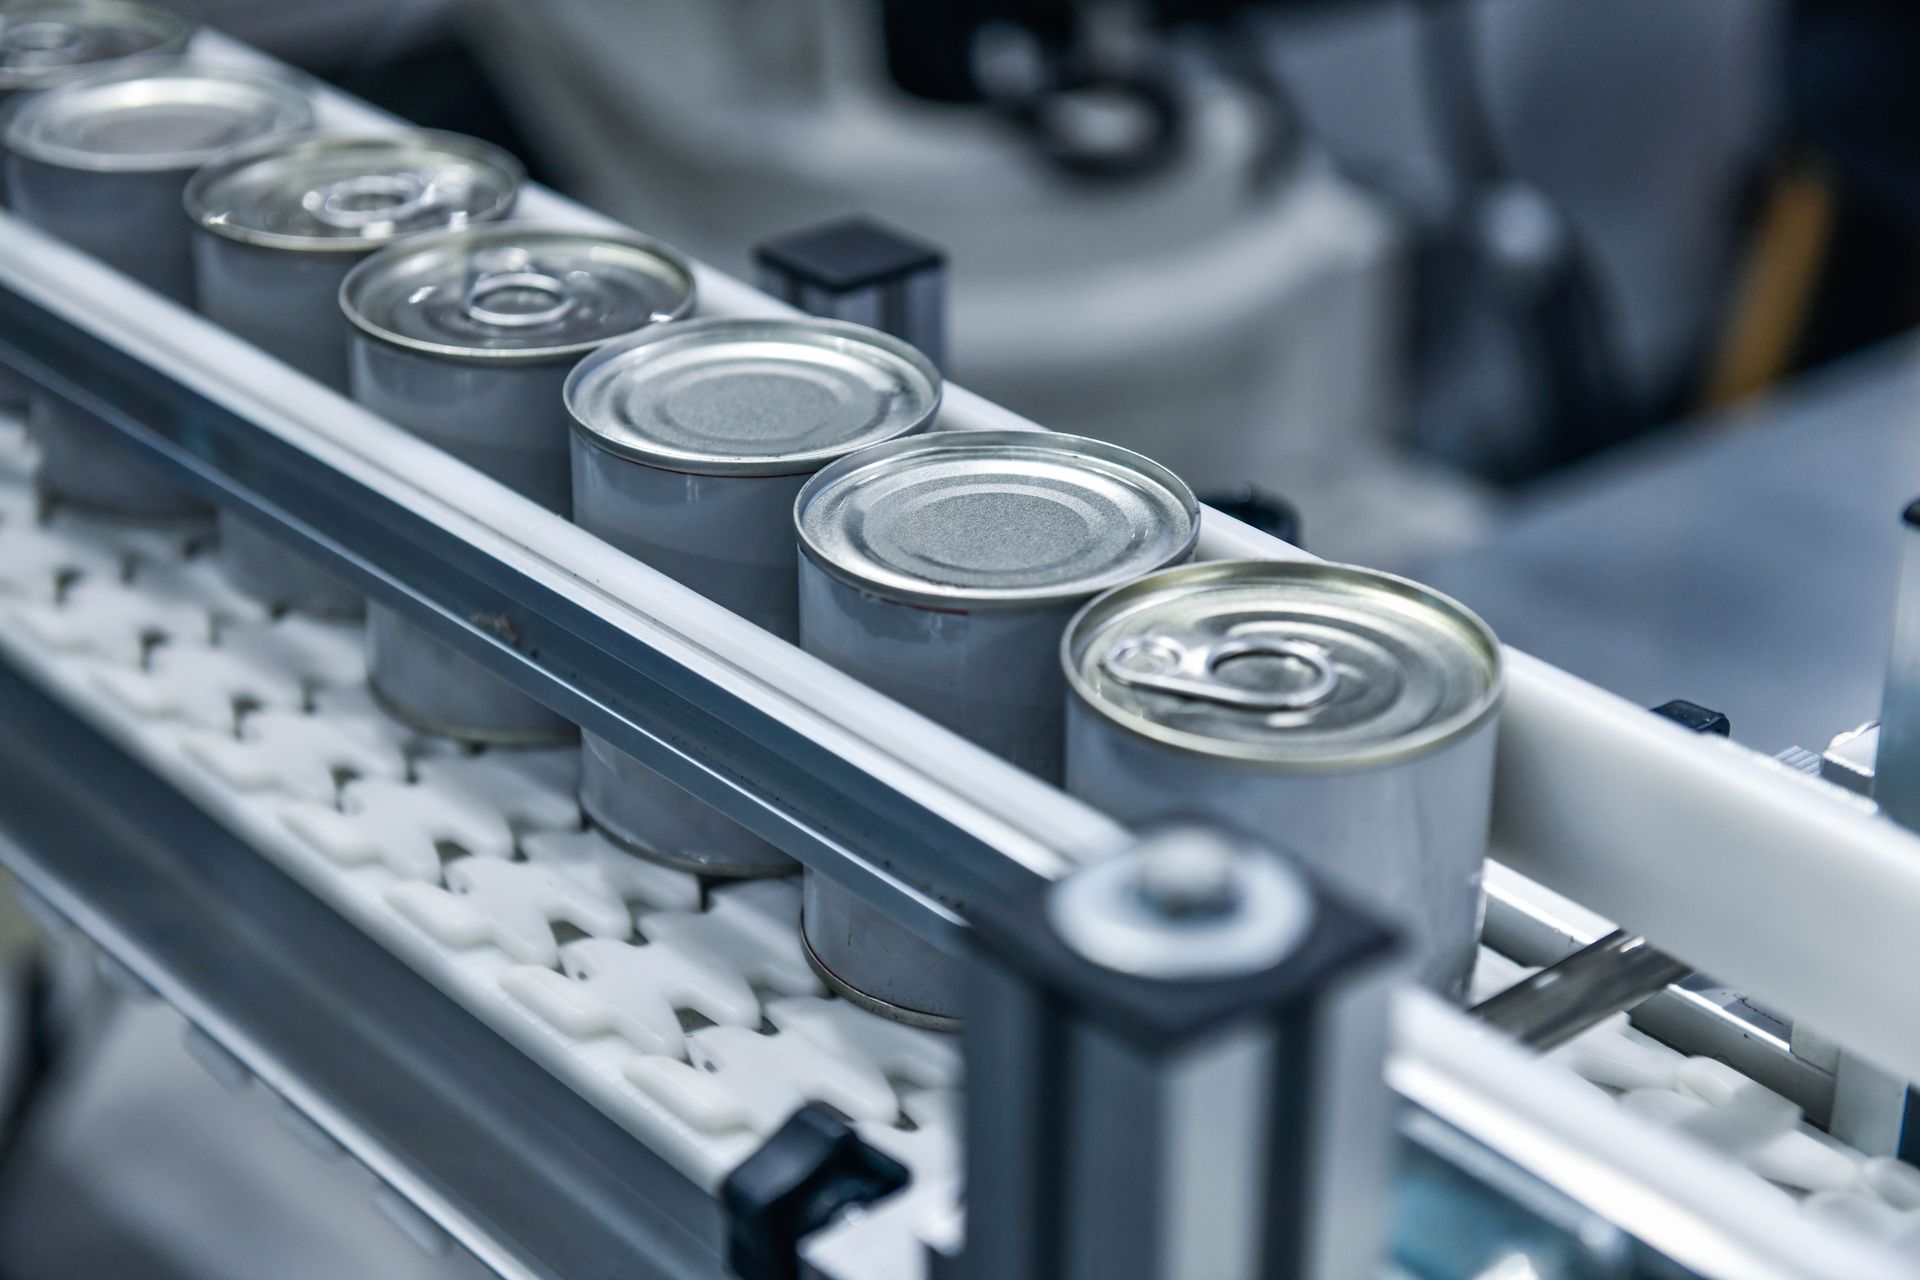
High-speed beverage lines often require servo-driven shrink wrappers that synchronize with upstream filling and downstream case packing to maintain throughput above 120 packs per minute, while slower batch operations benefit from adjustable tunnel speeds and modular film feed systems that accommodate package size variation without retooling.
Common Questions About Food Processing Packaging
Processing facilities packaging food and beverage products under refrigerated or sanitary conditions need packaging systems that meet regulatory and operational requirements without compromising line speed.
What makes a case sealer sanitary-design compliant?
Sanitary case sealers use stainless steel construction with smooth, crevice-free surfaces, sealed motor housings to prevent lubricant contamination, and quick-release components that allow complete disassembly and wash-down without tools or hidden spaces where product residue can accumulate.
How does cold-temperature stretch film differ from standard film?
Cold-temp films use polymer blends and plasticizers that remain flexible below 40°F, preventing the brittleness and cracking that occur when standard polyethylene films are applied or stored in refrigerated environments.
Why do shrink tunnels require precise temperature control for beverage multipacks?
Uneven or excessive heat causes package distortion, label damage, or incomplete shrinkage, while insufficient heat leaves loose film that doesn't provide structural support or tamper evidence, so tunnel airflow and element zoning must match the film type and package geometry.
What happens during a packaging line integration in a food plant?
Equipment is installed during scheduled downtime, connected to existing conveyors and utilities, then tested with actual product to verify speed synchronization, film tracking, and seal quality before resuming production, with all installation work following Good Manufacturing Practices to avoid introducing contamination.
How do you confirm that packaging materials meet FDA food contact requirements?
Materials are supplied with manufacturer certificates of compliance and tested formulations that meet FDA regulations for indirect food contact, and BRAVO SYSTEMS INC maintains documentation for all films, tapes, and adhesives used in food-zone applications in Battle Creek facilities.
Set up a production floor review to identify packaging materials and equipment that match your sanitary standards, temperature conditions, and line speed targets.